

SUNLU
SUNLU PETG-CF Carbon Fiber 3D Printer Filament 1.75mm 1kg Spool - Black
SUNLU PETG-CF Carbon Fiber 3D Printer Filament 1.75mm 1kg Spool - Black
SKU:IR0000026
In stock
Couldn't load pickup availability
- For Bulk Order Click Here
- Need Customer Support?
- Free Delivery Above 999/-
Note: In case you receive a damaged or faulty product, please return it in the original box with all foam and packaging. Returns will not be accepted if further damage occurs due to improper packing.
If you order a product that is currently in Preorder, and the price of that item increases in the future, you will be required to pay the difference in price.
For refund/return/replacement, call us at +91 95995 94520 or email us at support@rees52.com
Delivery Time
Delivery Time
- Delivery time with the Express Shipping option is 2-3 working days, and with the Standard Shipping option is 5-6 working days. It varies based on location, reliant on courier services.
- Delivery time if the order item is on Preorder Status is 15-20 working days.
COD (Cash on Delivery)
COD (Cash on Delivery)
Cash on Delivery is currently unavailable for new orders
Existing COD Orders Only
- For COD you have to pay extra charges of Rs 350/- before the shipment. (We will share the company QR Code, UPI ID or Account details for the same)
The REES52 Promise
The REES52 Promise
We want you to build, not worry. Here is exactly what happens if something goes wrong with your order.
Dead on arrival or defective? We replace it.
If your item is dead on arrival or has a manufacturing defect, tell us within 7 days of delivery. Email support@rees52.com with your order number and a short video or a couple of photos showing the problem. Our team will get back to you within 24 hours and arrange a free pickup from your doorstep - you never pay return shipping for a defective item. Once we verify the issue, your replacement ships out right away. If the item is out of stock, you get a full refund instead.
Refunds, with real timelines.
- Approved refunds go back to your original payment method within 6-7 working days.
- Missing item in your package? Tell us within 7 days with photos of what arrived and the parcel label. Once confirmed, the refund for the missing item reaches you in 2-3 working days - or we ship the missing piece free, your choice.
- Every refund comes with a reference number by email or WhatsApp, so you can track it with your bank instead of chasing us.
Wrong item or not as described?
Email us your order number and a photo of what you received. We arrange the return pickup, and ship the correct item as soon as the return is on its way. Prefer your money back instead? That is fine too - full refund, same 6-7 working day timeline.
About lead times on some products.
A few items on rees52.com are sourced from our overseas partner warehouses and are not sitting on our shelf. Those products show a lead time of about 20-25 working days on the product page, before you pay. If you order one, we keep you posted as it moves. Changed your mind while waiting? You can cancel any time before dispatch and get a full refund within 6-7 working days. No cancellation fee, no questions.
Talk to a human.
Email support@rees52.com or call/WhatsApp +91 95995 94520, Monday to Saturday, 10:30 AM to 7:00 PM. Real people, order number in hand, actual answers.


SUNLU PETG-CF Carbon Fibre 3D Printer Filament - Black, 1.75mm, 1kg
SUNLU PETG-CF10 is a carbon fibre reinforced PETG filament infused with 10% chopped carbon fibre, built for parts that need real strength and stiffness. It is made for industrial applications such as drone frames, tools, automotive components and structural parts, while printing almost as easily as regular PETG. This 1kg spool of black 1.75mm filament suits engineering workshops, drone builders, robotics teams and serious hobbyists across India.
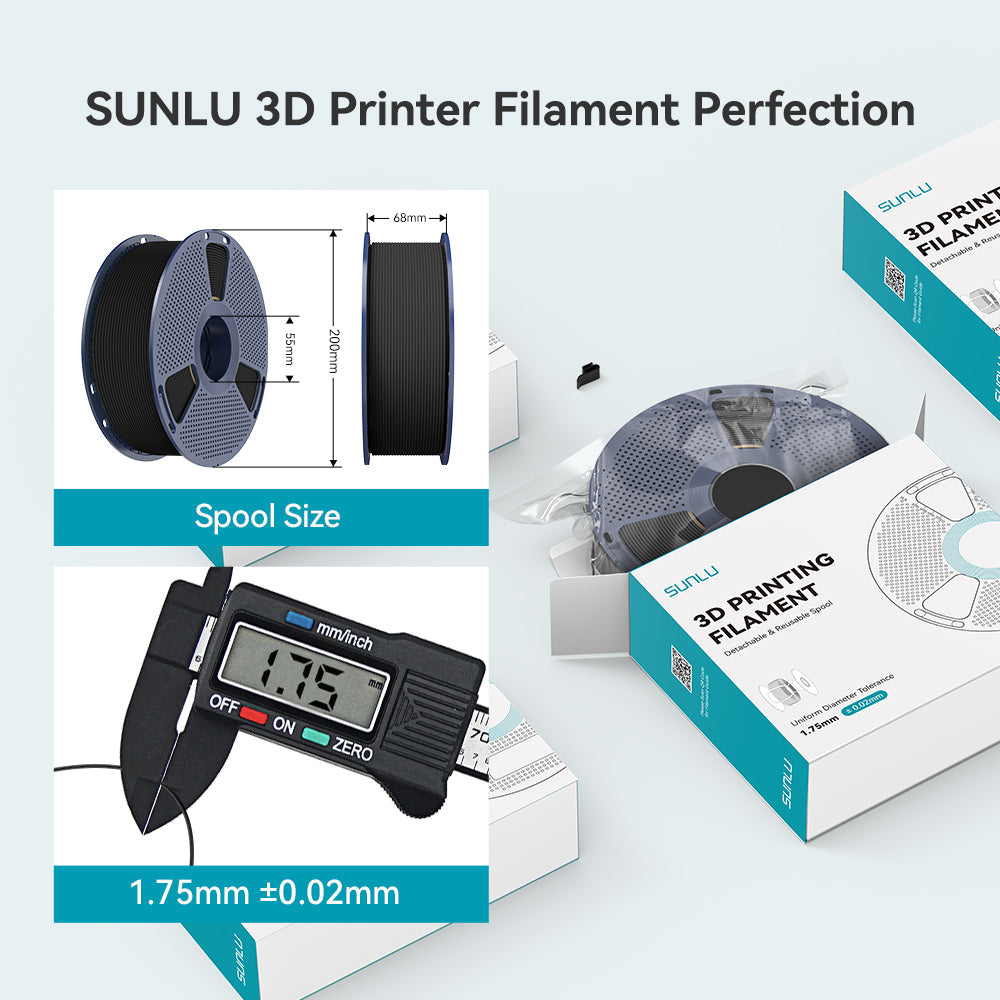
The carbon fibre reinforcement raises stiffness and impact strength to 7 ± 2 kJ/m² while cutting the creep and warping seen in plain PETG, so load-bearing parts hold their shape over time. Prints come out with a premium matte finish that hides layer lines and needs no post-processing. Diameter is held to a tight 1.75 ± 0.02 mm tolerance for stable extrusion, and the filament runs on most FDM printers - Bambu Lab, Creality, Anycubic, Prusa, Elegoo and more.
Key Features
{CF_FEATURES}Technical Specifications
| Material | PETG + 10% carbon fibre (PETG-CF10) |
|---|---|
| Colour | Black |
| Diameter | 1.75mm (± 0.02mm tolerance) |
| Net weight | 1kg spool |
| Nozzle temperature | 240-250°C (up to 150mm/s) |
| Bed temperature | 50-70°C |
| Tensile strength | 32 ± 4 MPa |
| Flexural strength | 55.5 ± 5 MPa |
| Notched Izod impact strength | 7 ± 2 kJ/m² |
| Elongation at break | 14 ± 3% |
| Density | 1.23 g/cm³ |
| Melt flow index | 5.7 ± 1.5 g/10 min |
| Heat deflection temperature | 71 ± 3°C |
| Shore hardness | 71 HD |
| Recommended retraction | 0.8-1.2mm at 30mm/s |
What is it good for?
Drone frames and RC parts, functional prototypes, tooling, jigs and fixtures, automotive under-bonnet components, robotics structures, machine brackets and any part that needs stiffness, impact resistance and a clean matte black finish.
In the box
- 1 x SUNLU PETG-CF10 carbon fibre filament spool, Black, 1.75mm, 1kg net weight
Good to know
- Carbon fibre is abrasive - a hardened steel or ruby nozzle is strongly recommended (a brass nozzle will wear quickly).
- Dry at 60-65°C for 4-6 hours if the spool has absorbed moisture.
- An enclosure is not required, but keep the print away from drafts for best layer bonding.